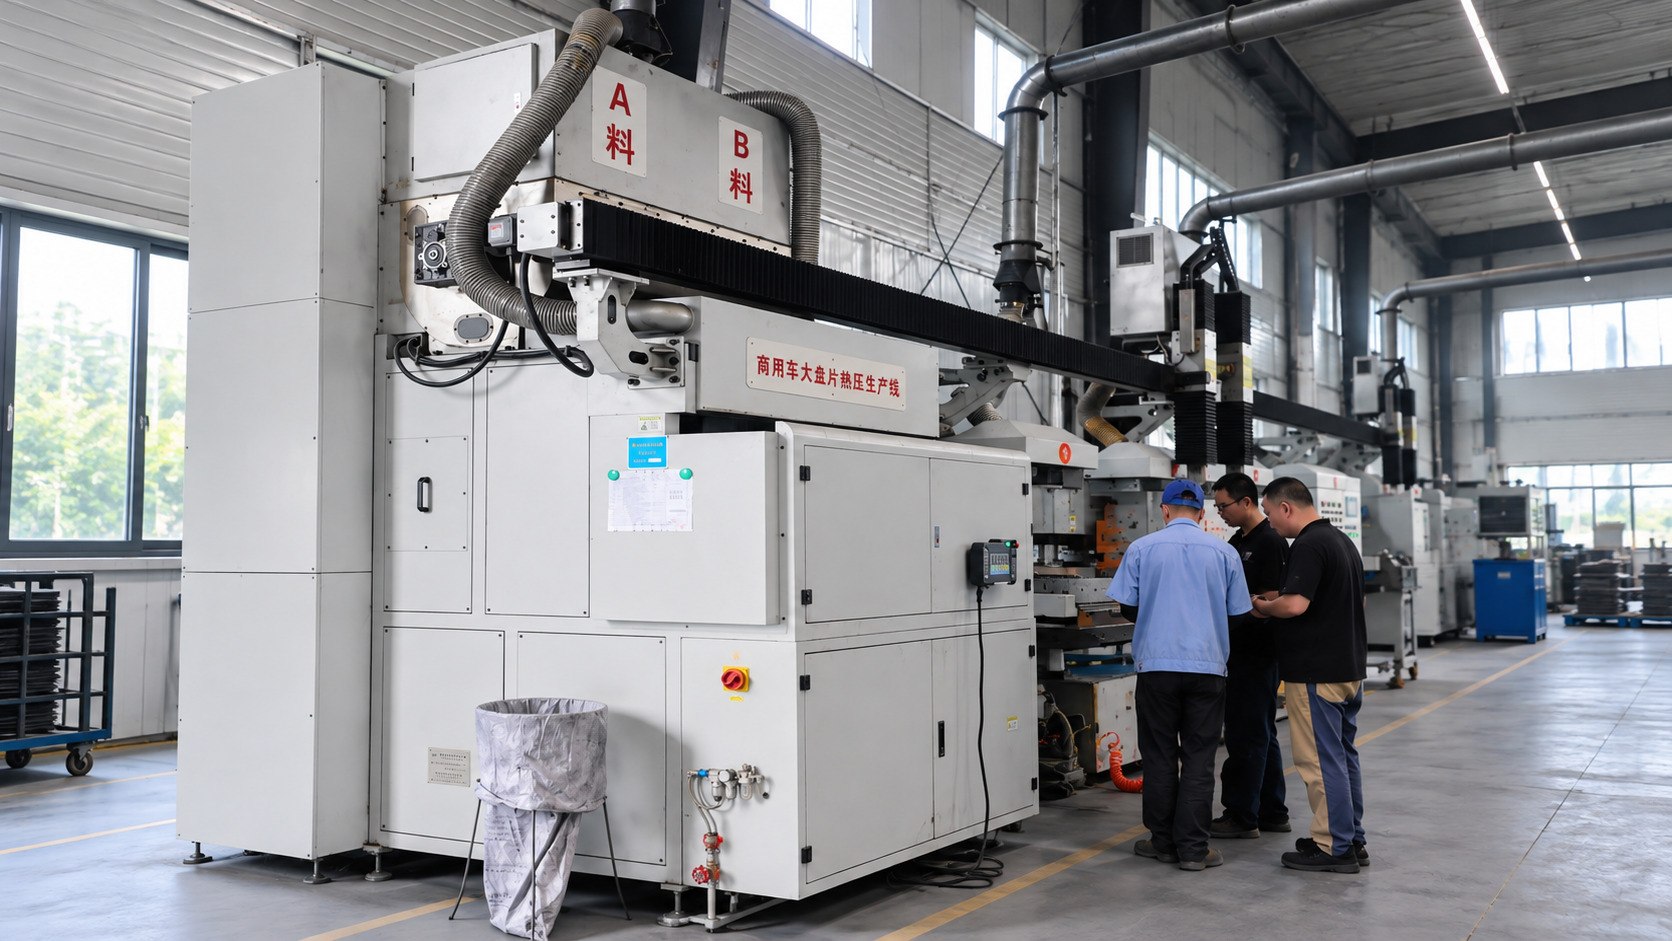
The production of advanced friction formulas, such as the F, JGW, LSL, and WZSD series, begins with the fully automatic batching machine, where raw materials are put into the mixer and thoroughly stirred to create the highly precise friction material mixture.
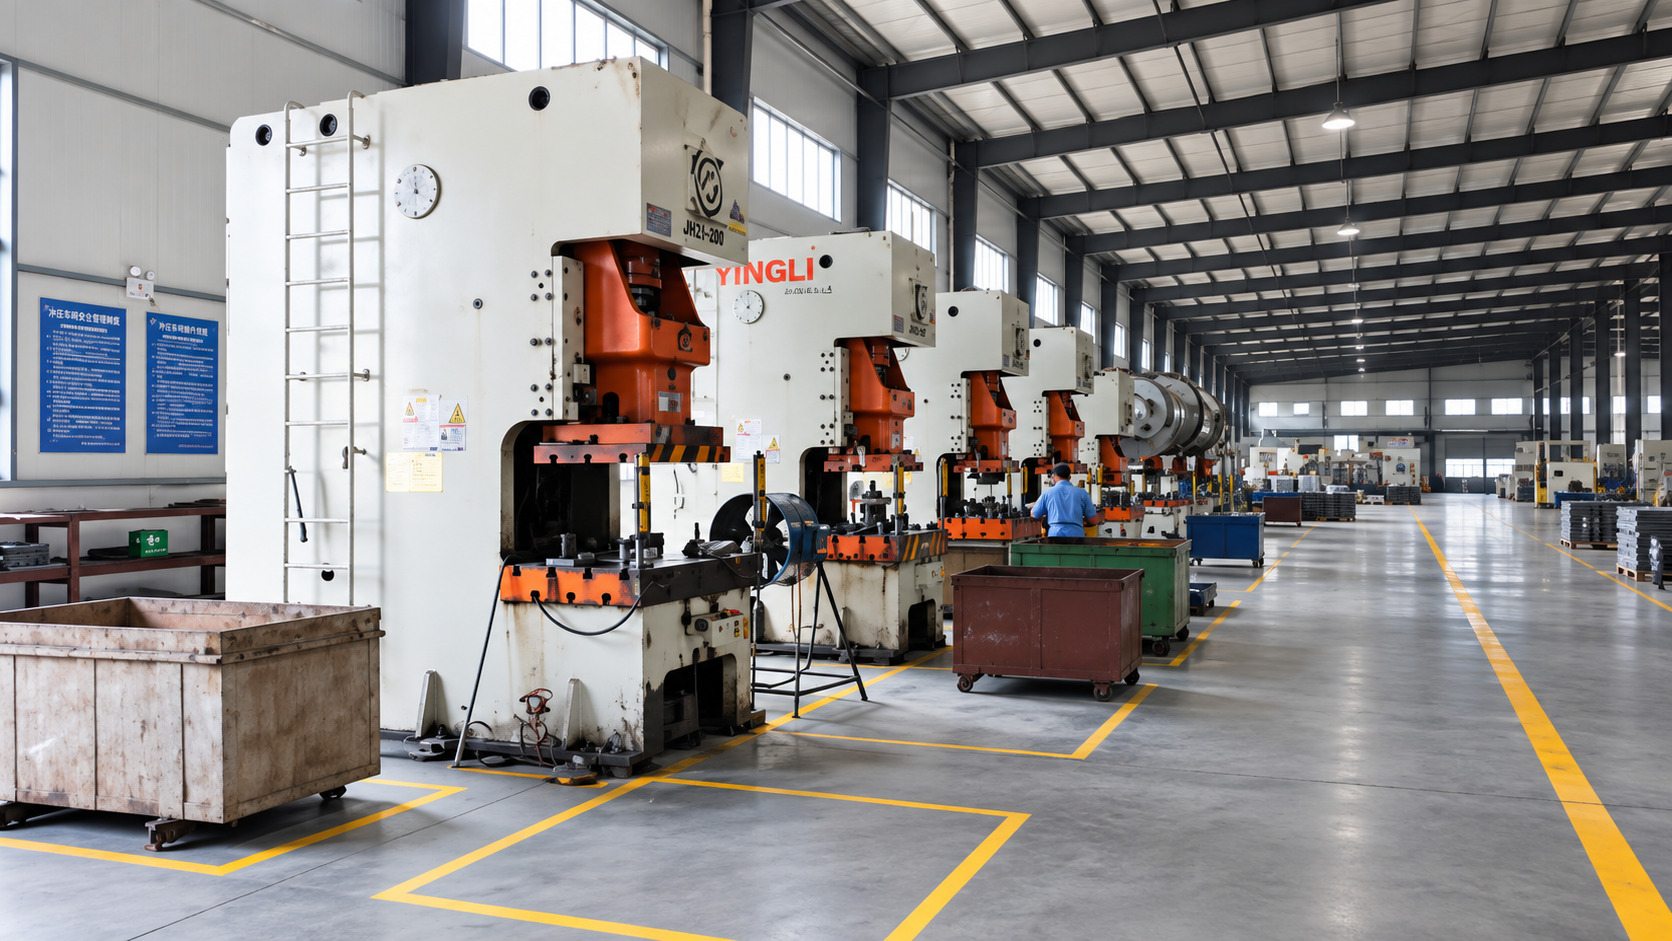
In the steel backing stamping stage, steel coils are cut and stamped into the shape of the brake pad's steel backing. Operators use a degreaser to remove oil from the surface, apply a specialized adhesive evenly on the reverse side, and air-dry it.
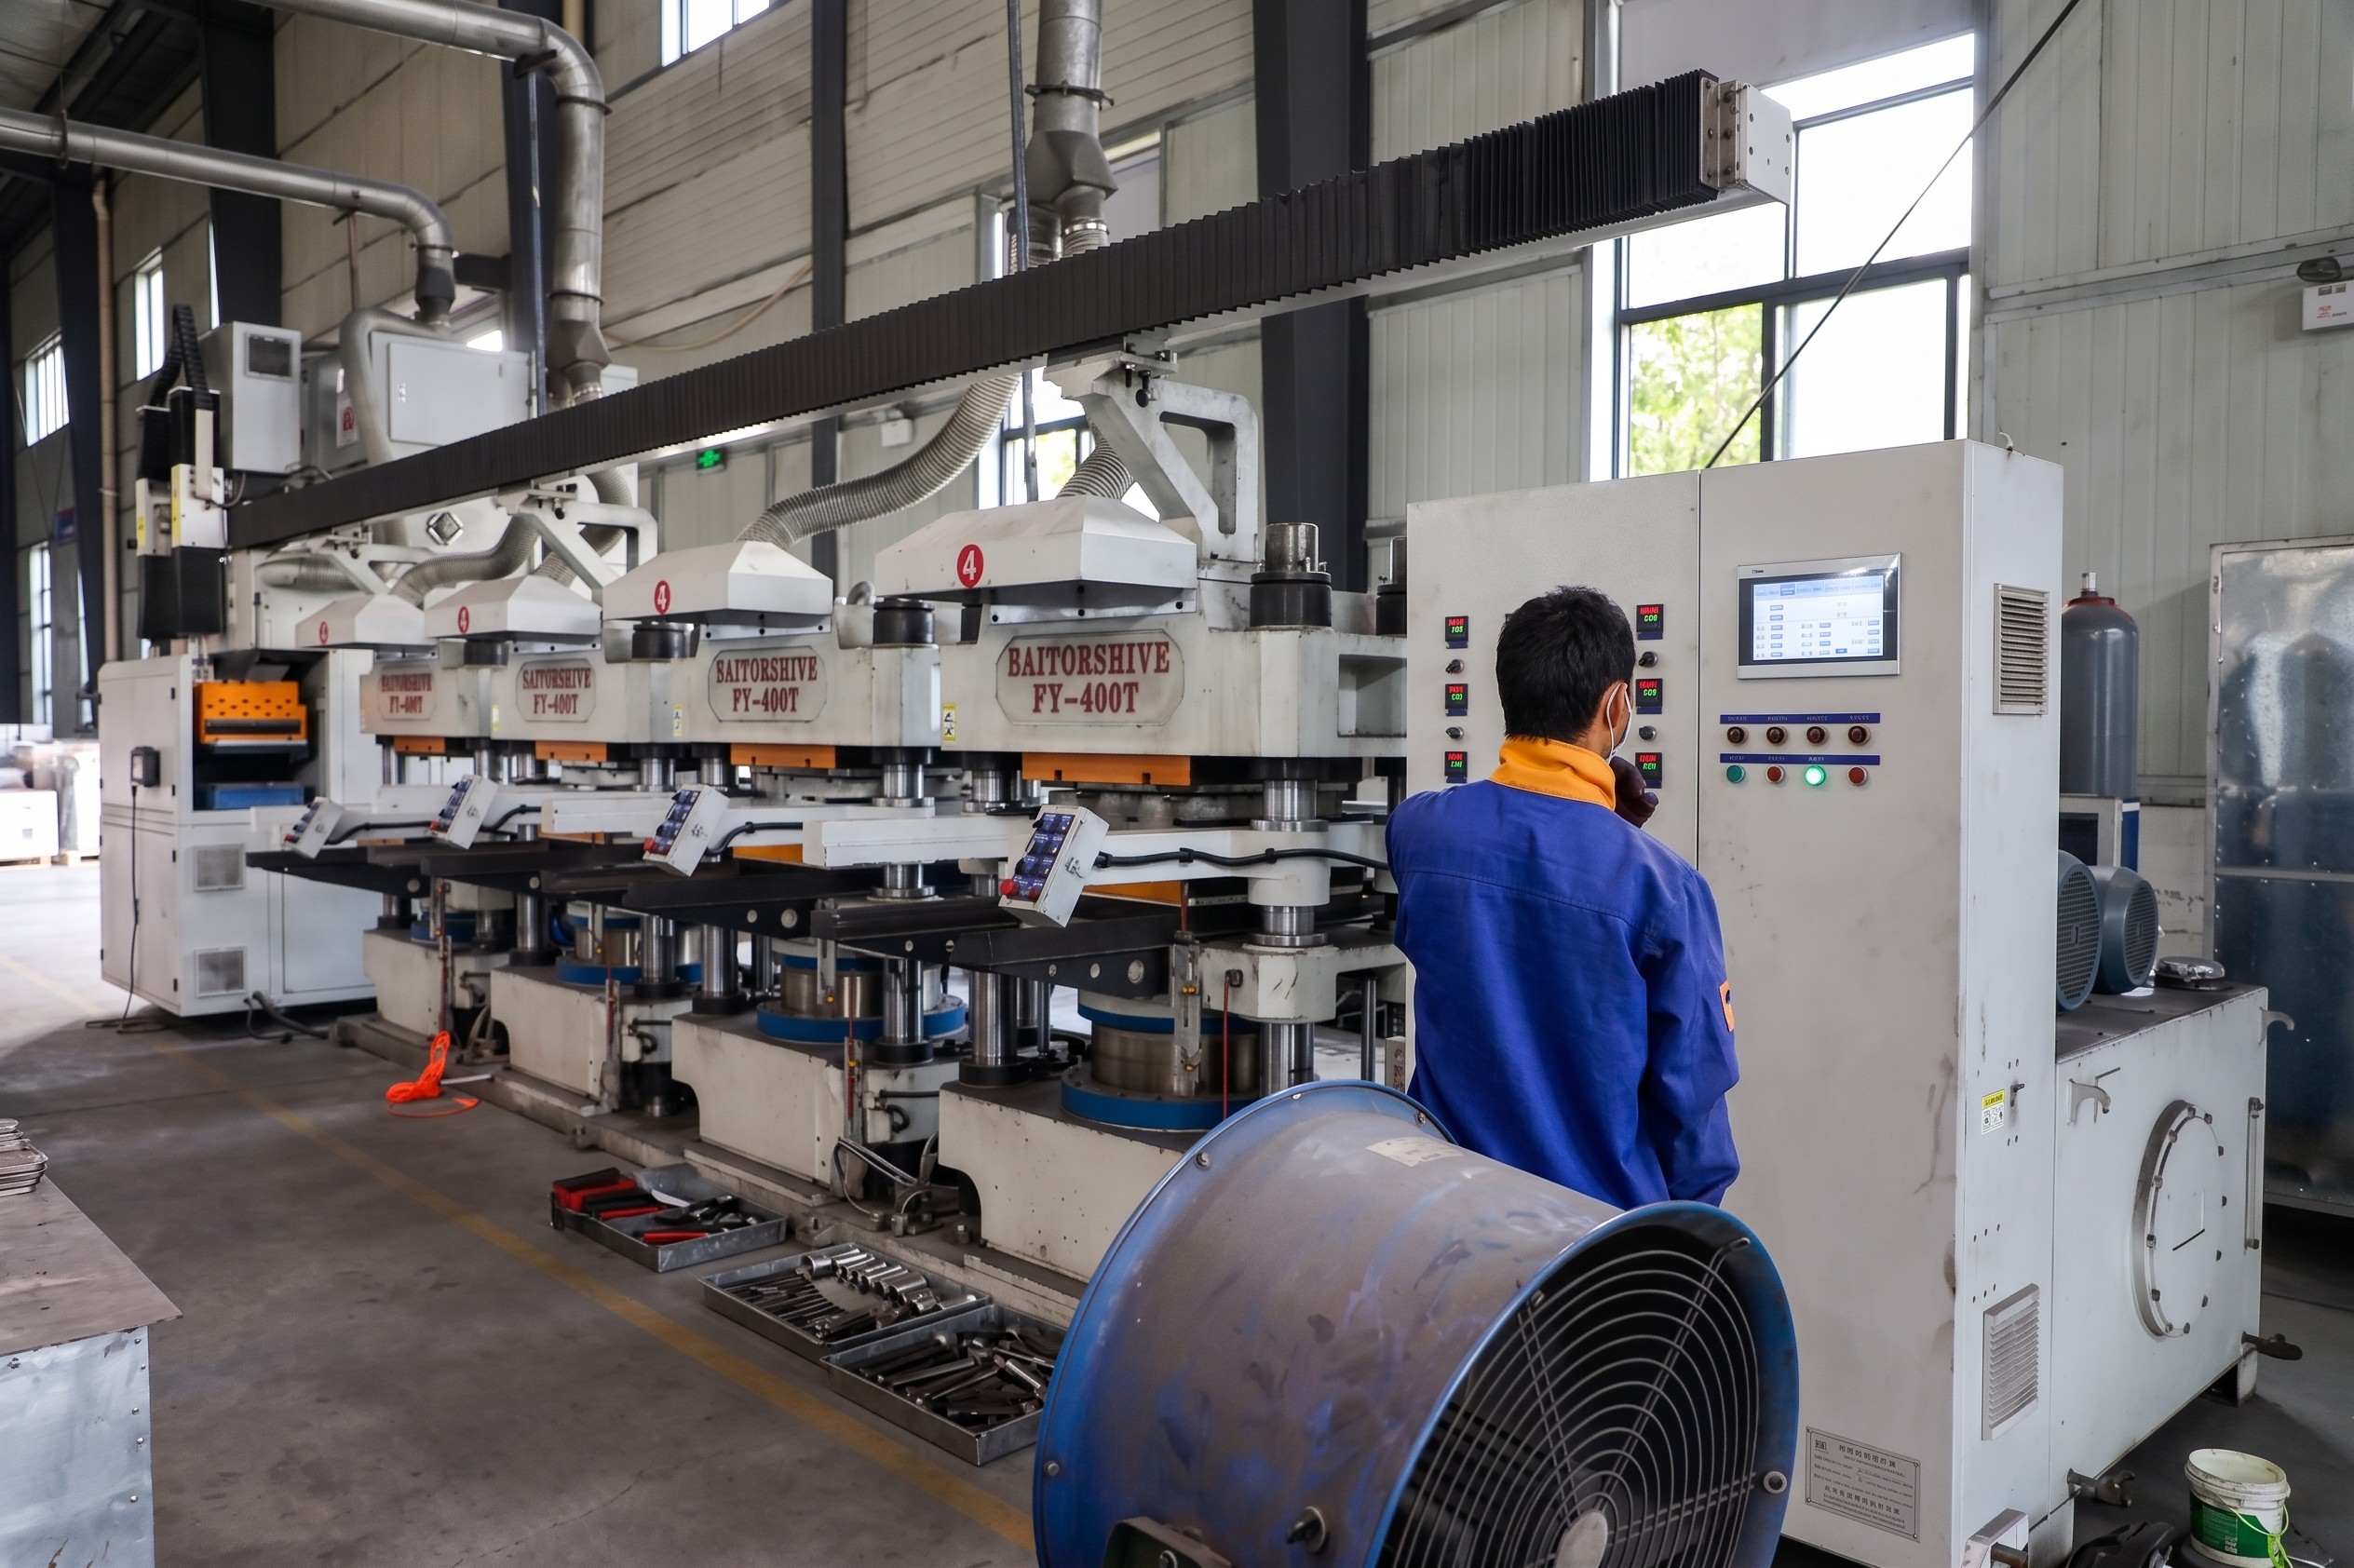
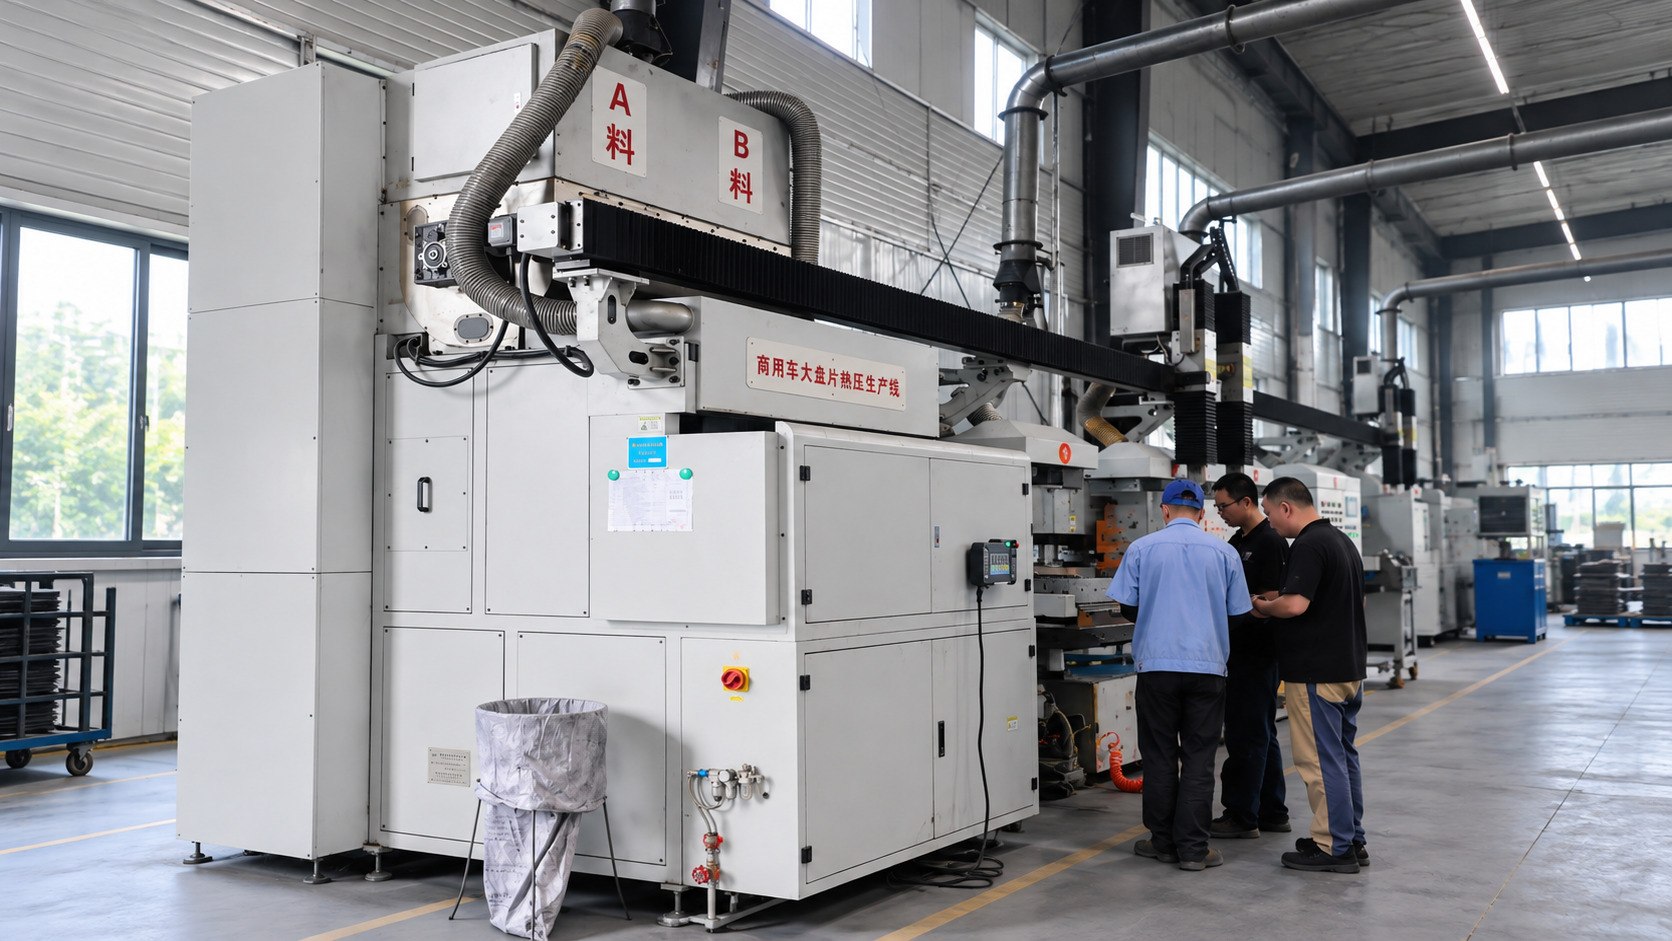
To shape the specific formula blocks, a precise amount of the mixture is weighed and poured into the mold, then hot-pressed together with the glued steel backing at about 170°C under 7-18 MPa of pressure for 200 seconds.
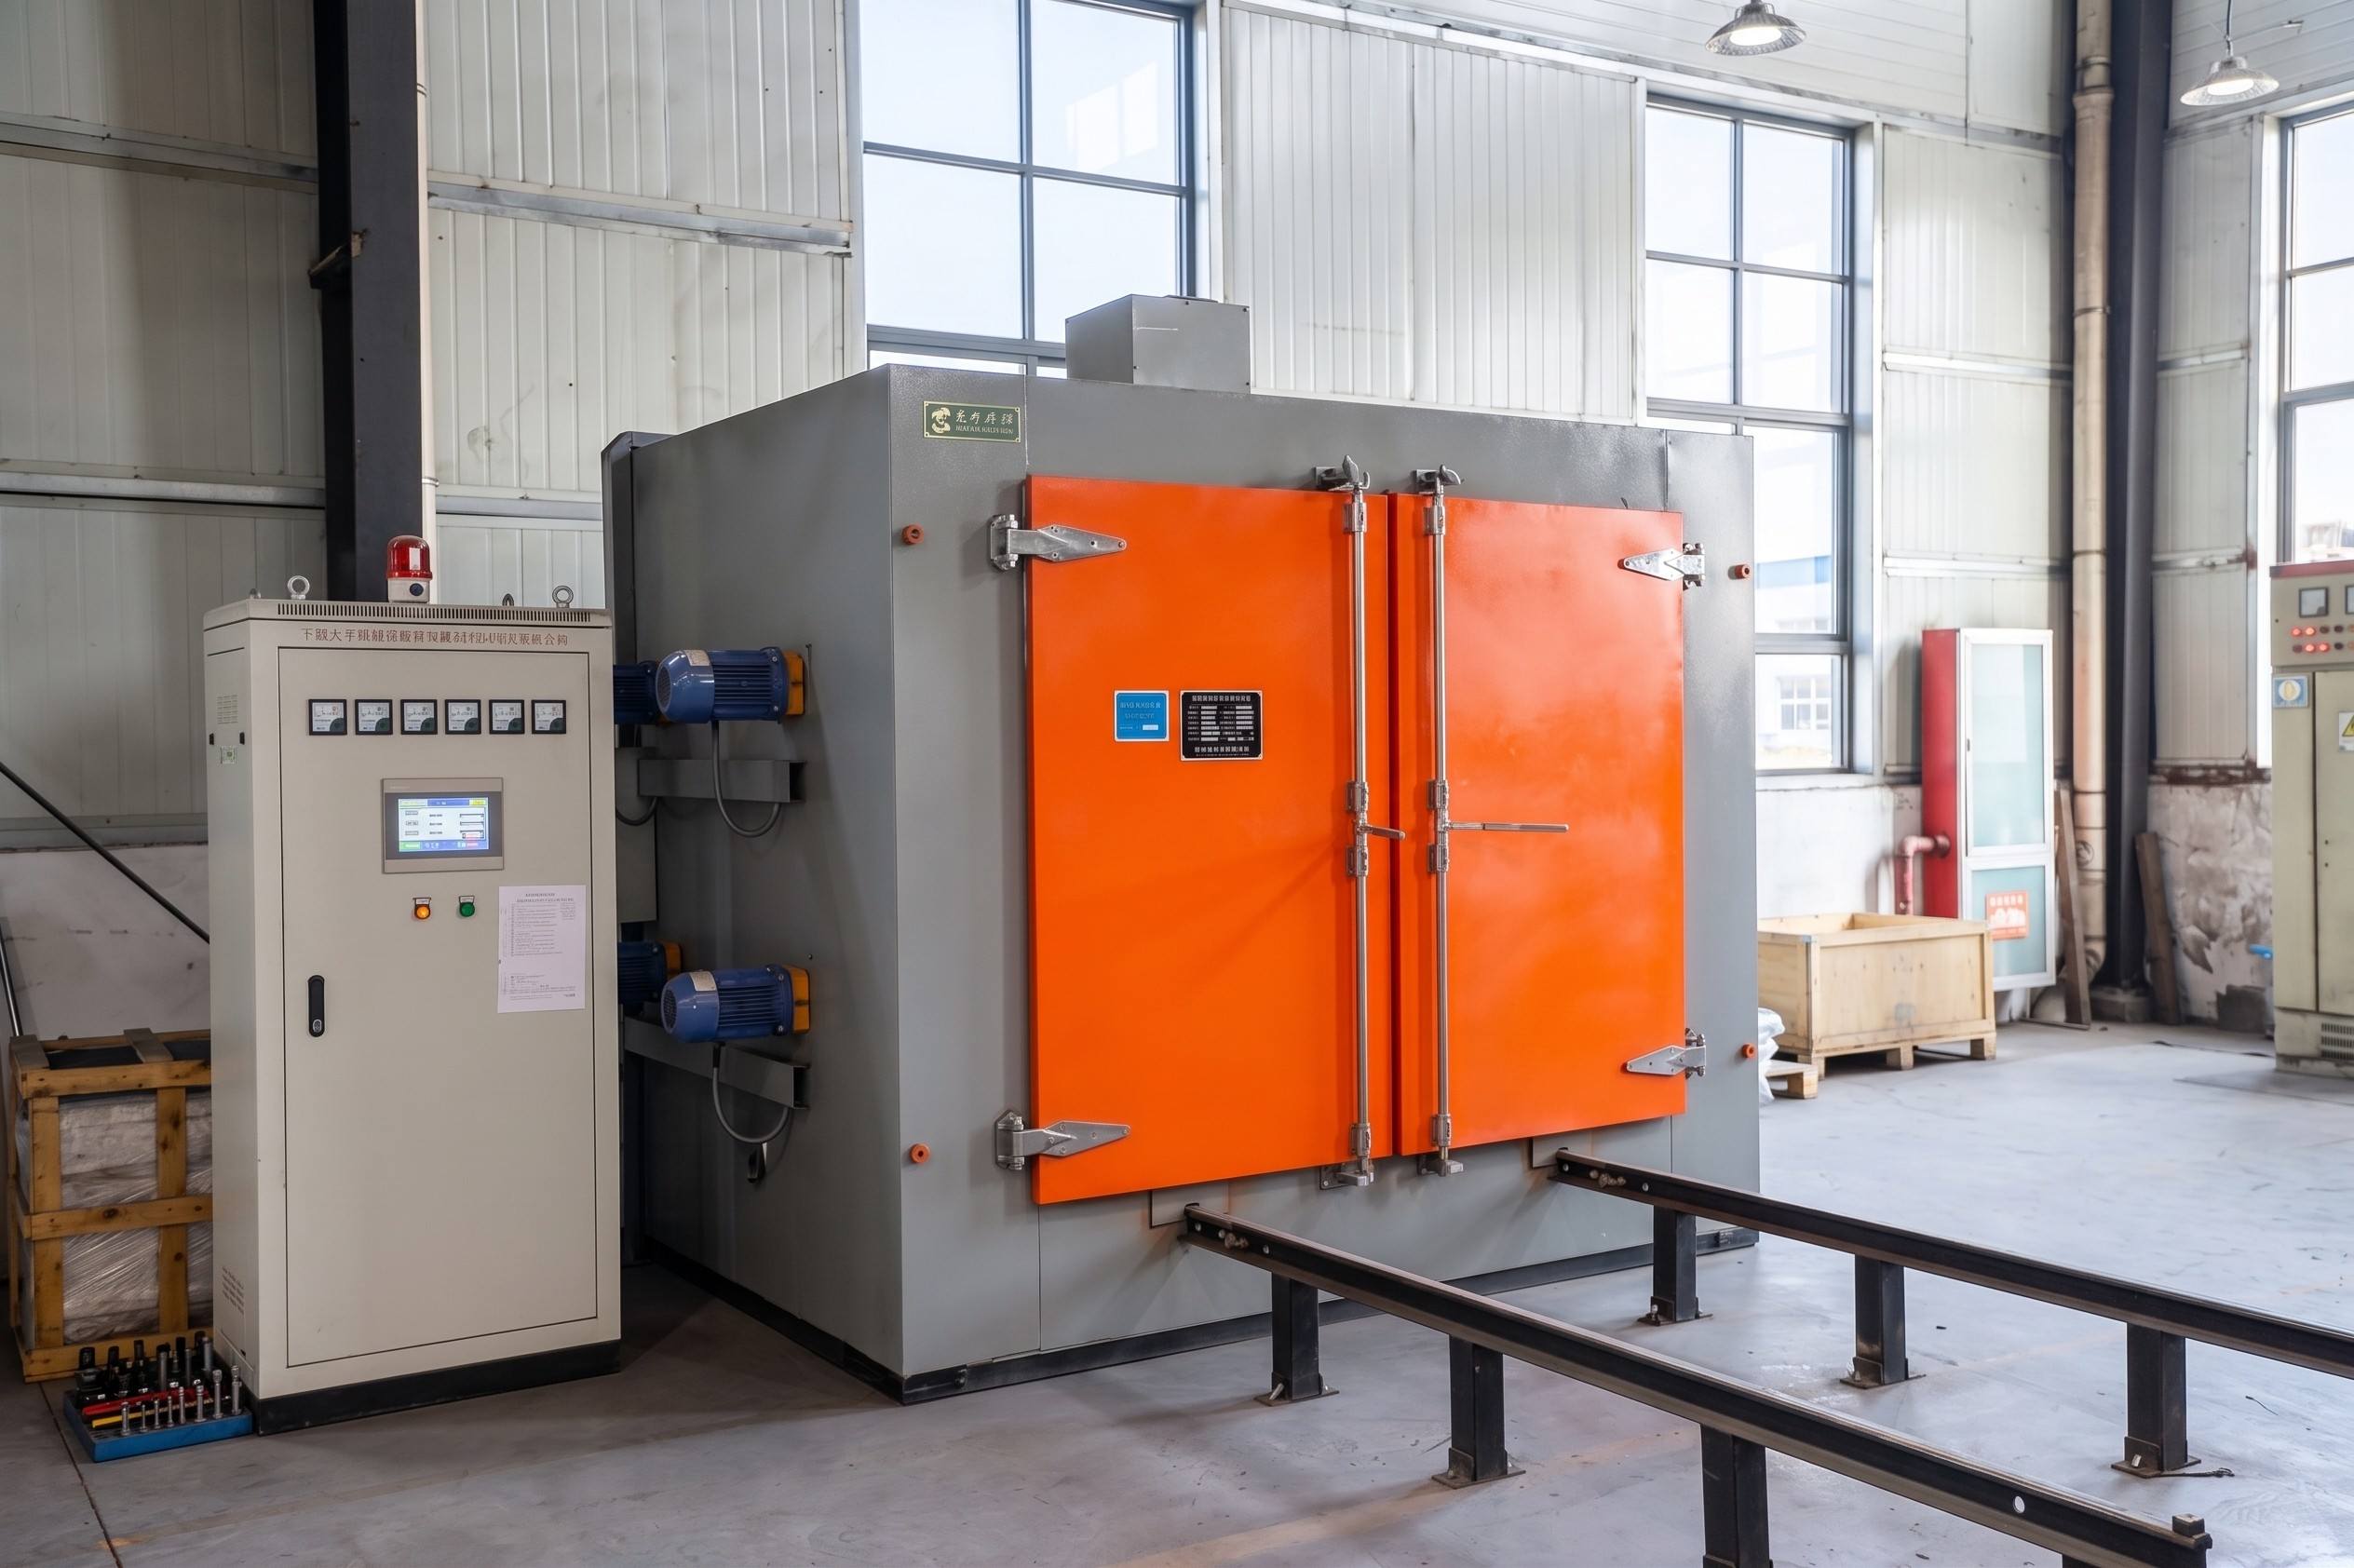
During heat treatment, the semi-finished products are sent into an oven for step-by-step baking between 0 and 170°C. This crucial step allows the resin to completely cure, stabilizing the unique friction performance of the F, JGW, LSL, and WZSD series.
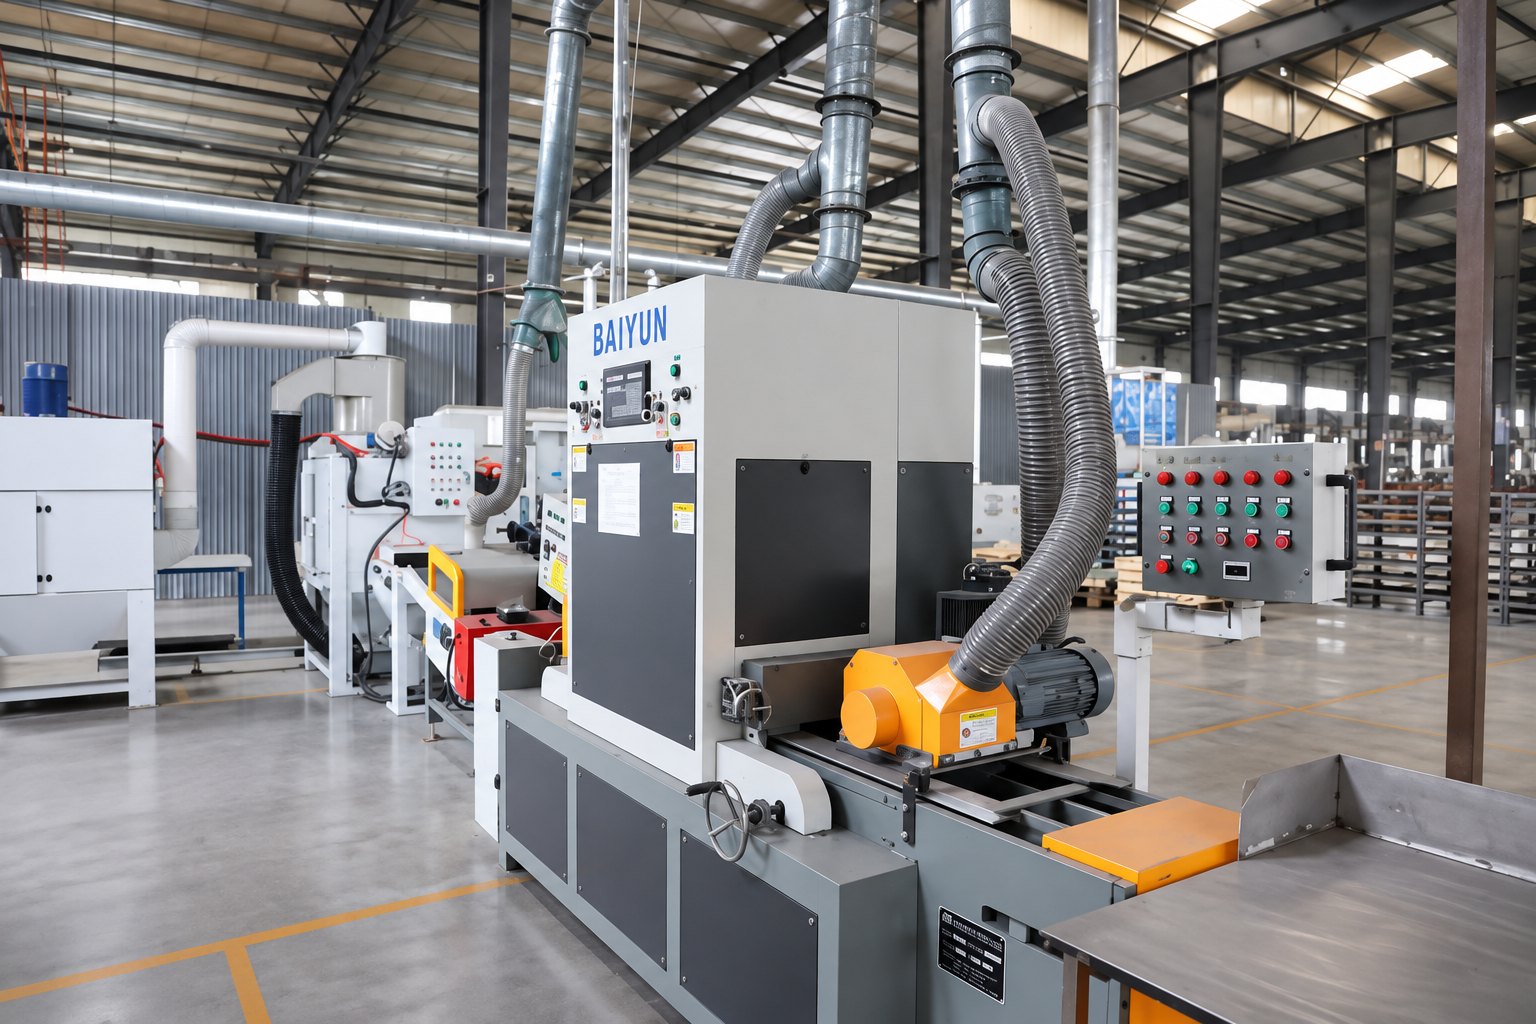
The grinding process utilizes a combination grinder to finely grind the surface of the friction material, ensuring it meets the stringent requirements for thickness, parallelism, and surface finish. Furthermore, some products require slotting or chamfering during this stage.
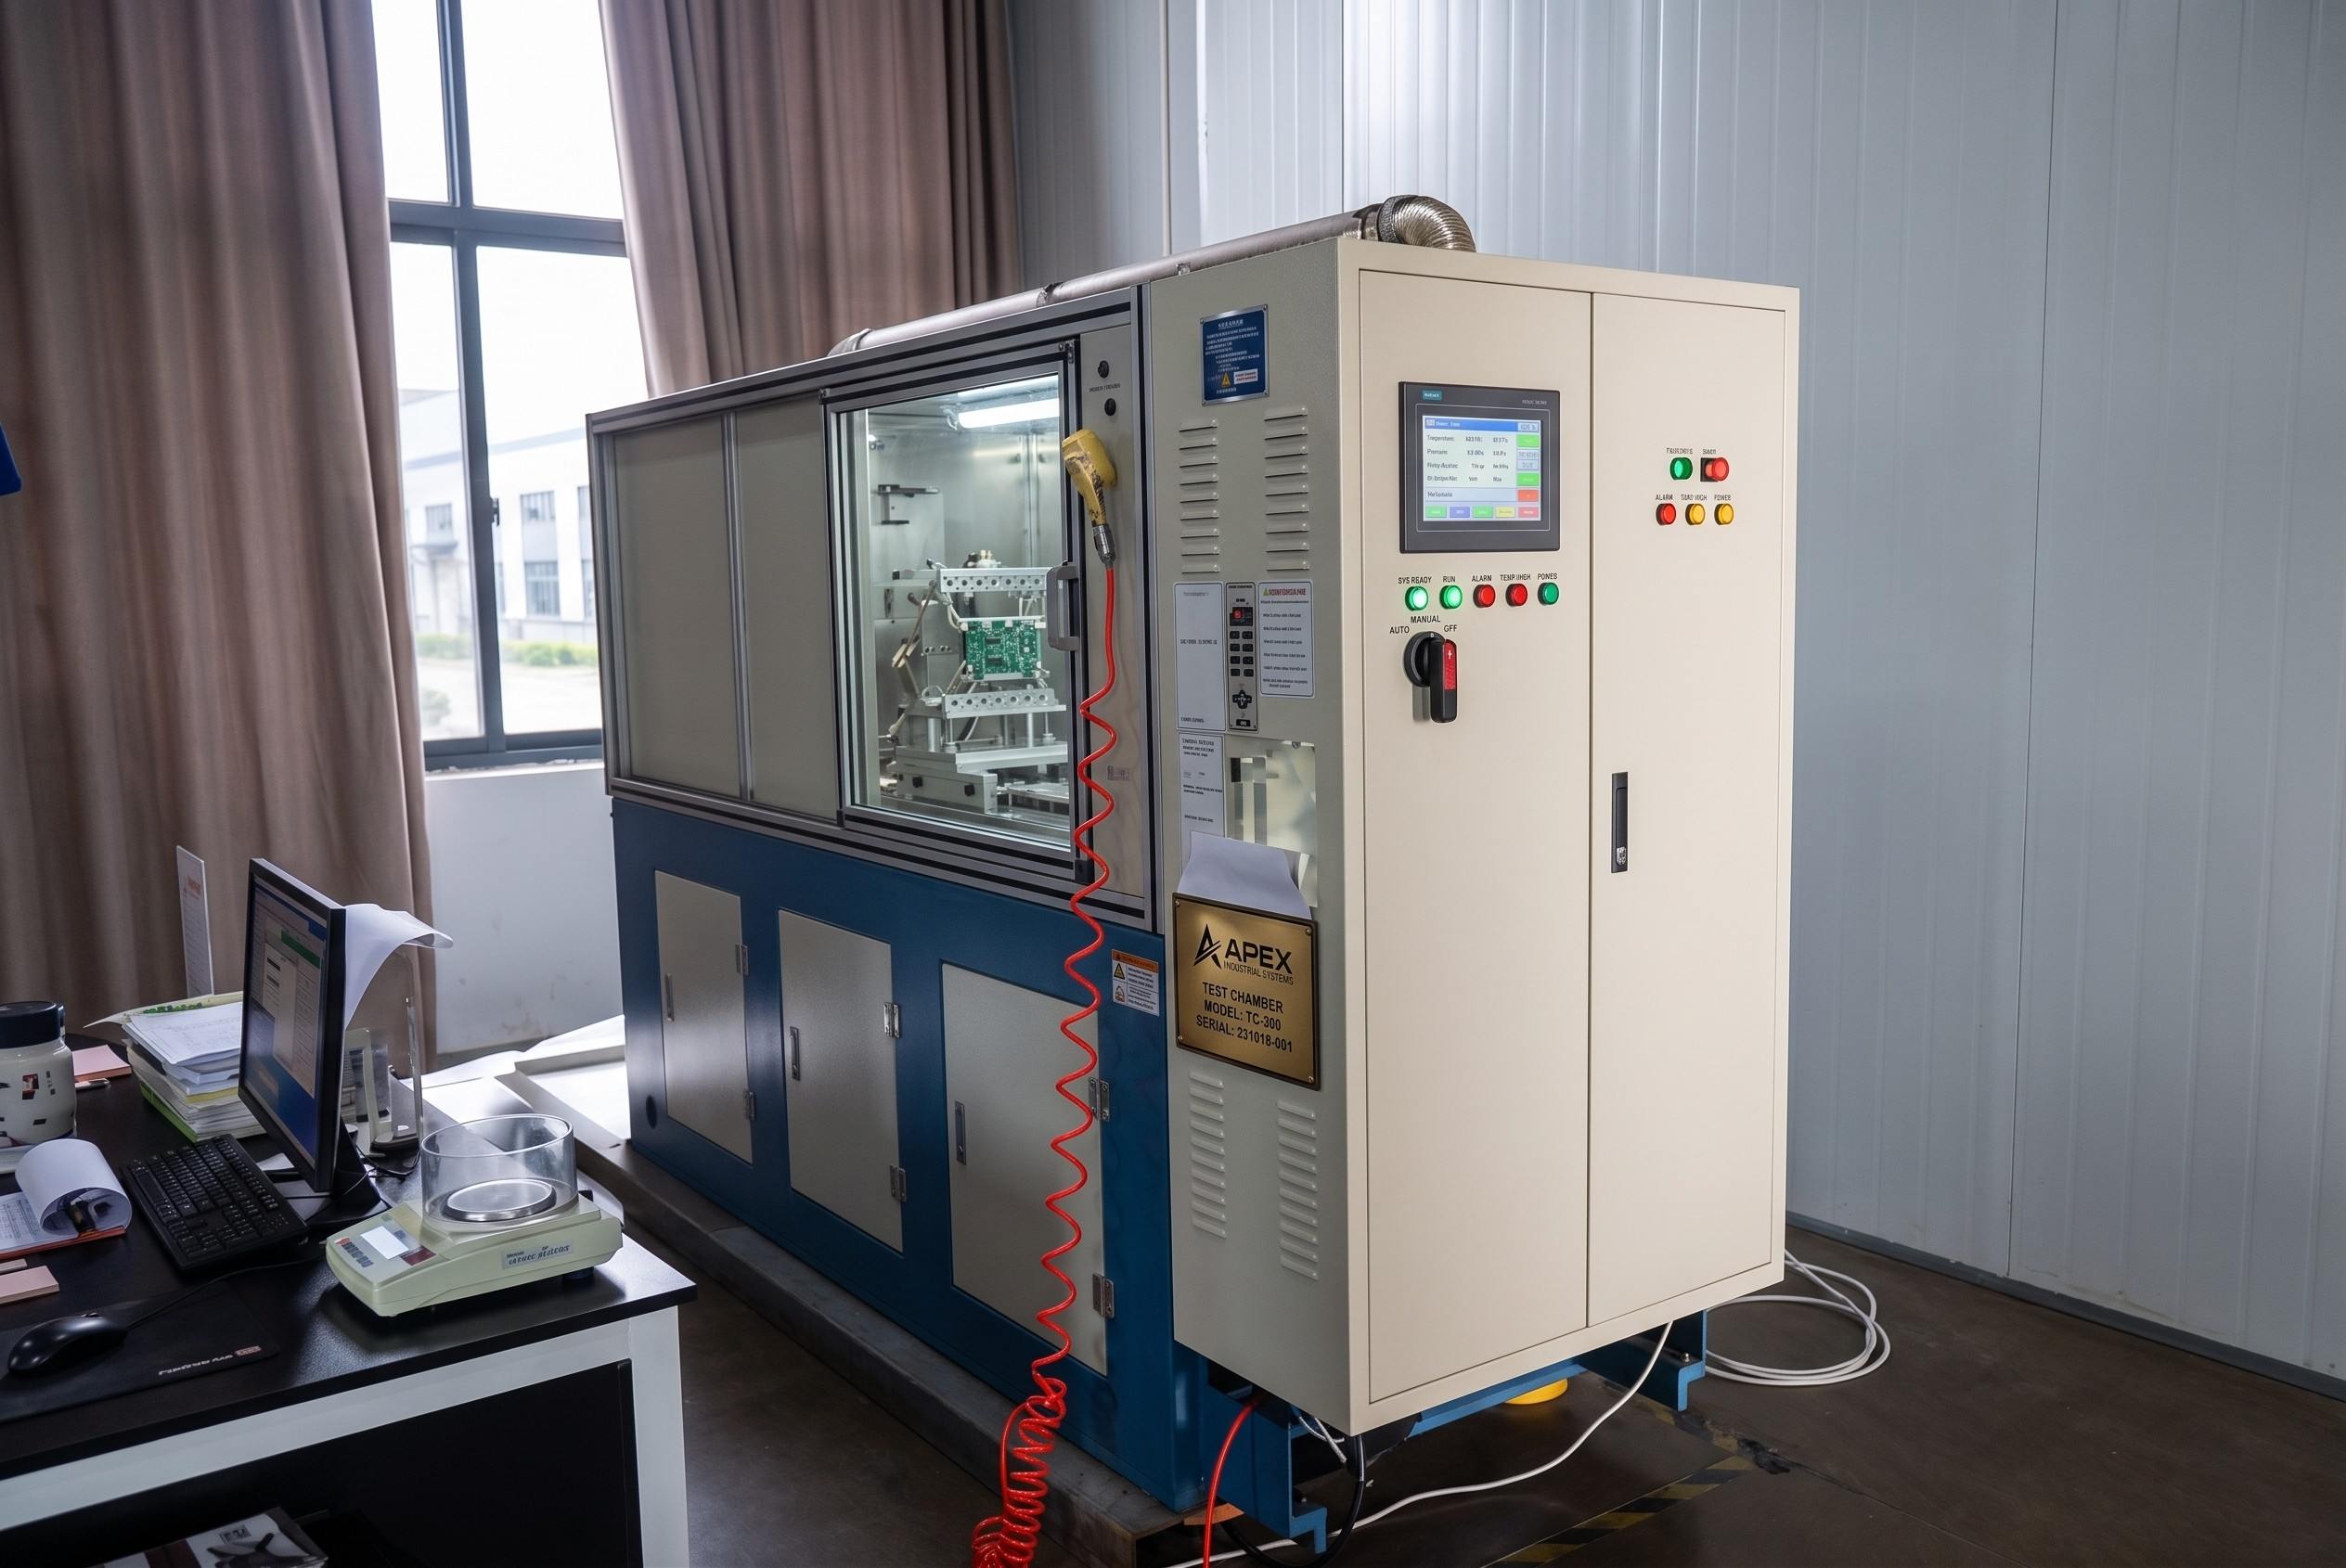
To guarantee the reliability of these advanced brake linings, every batch goes through testing using a drag testing machine, ensuring that each batch meets the qualification standards before leaving the facility.
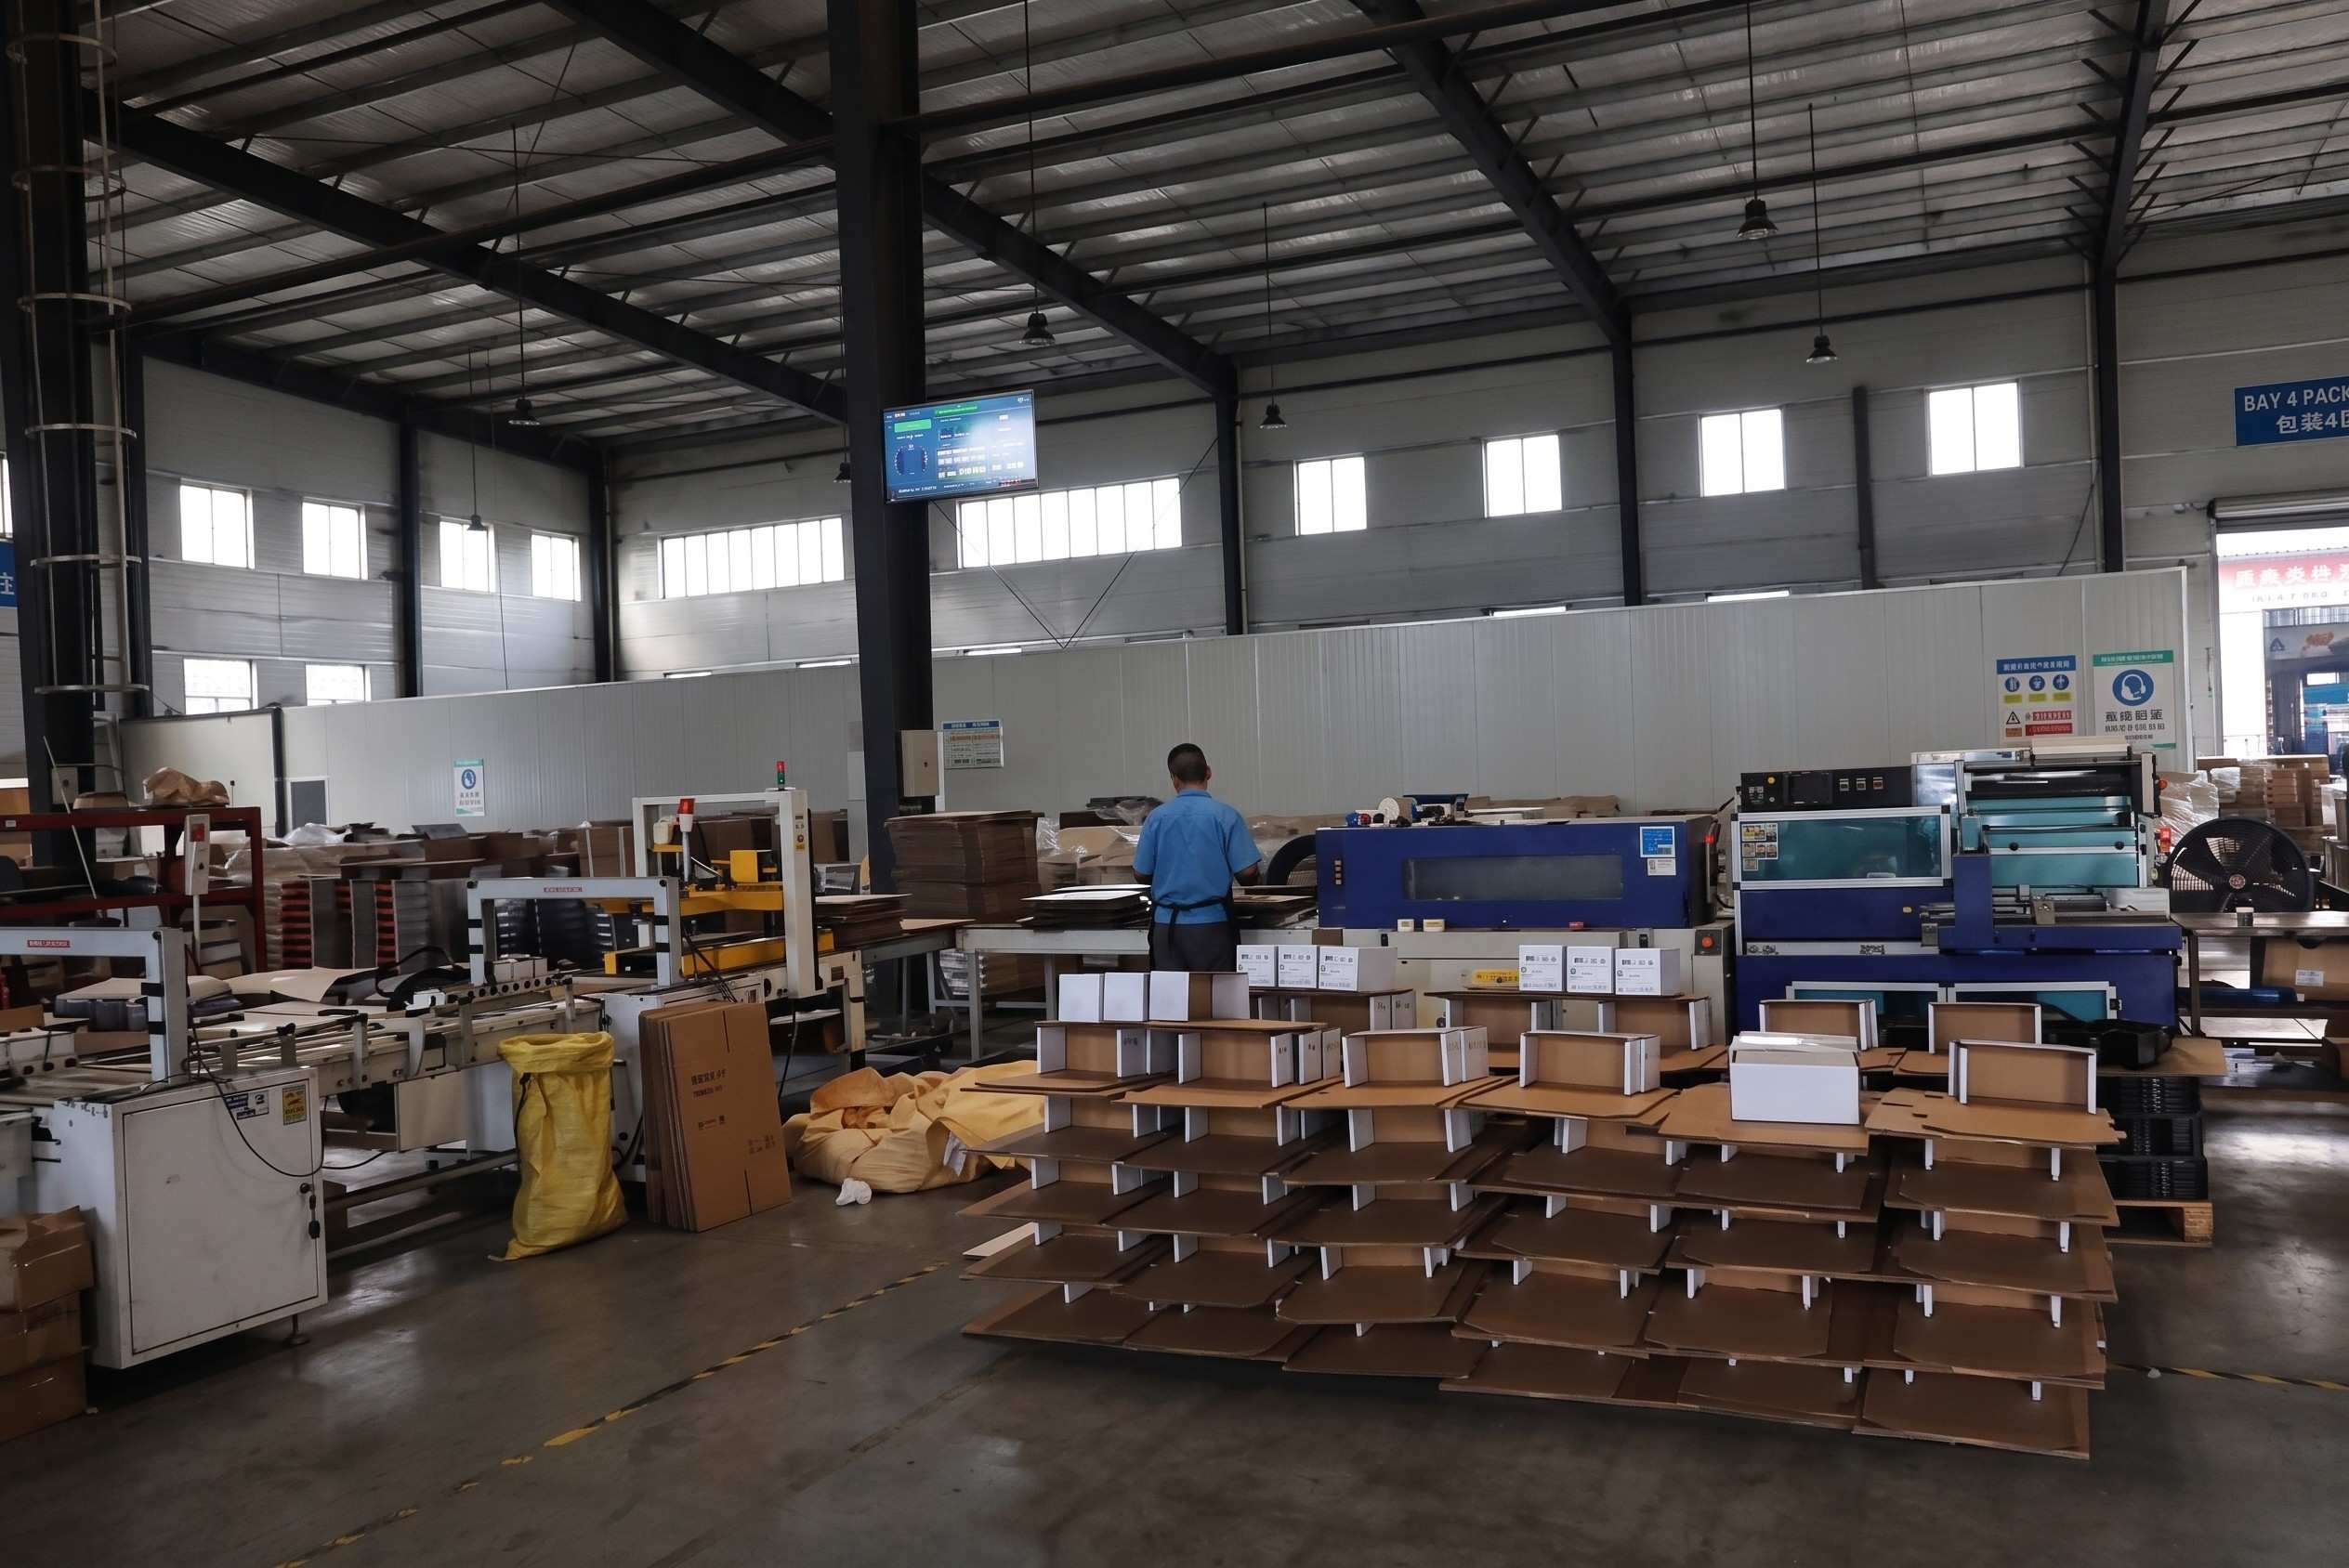
The final step is coding and packaging, where the production batch number and specific model (such as F, JGW, LSL, or WZSD series) are printed on the product. Following this, the products are plastic shrink-wrapped and stored in the warehouse.
Contact TOUGHPRO today. Our experienced sales and engineering team will provide professional technical support and competitive quotations within 24 hours.